 |


| Quantity: | |
|---|---|
Main Features
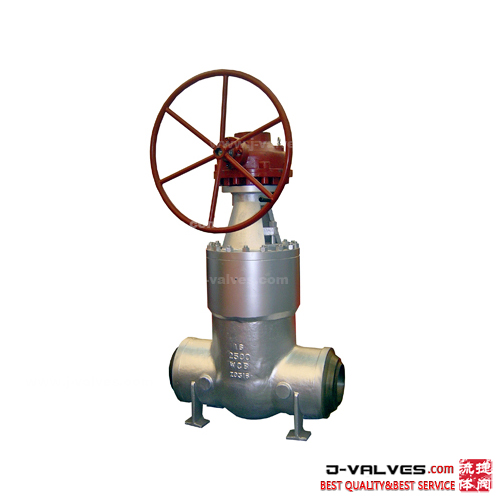
Pressure Seal Design: The bonnet adopts a pressure seal structure. As the system pressure increases, the sealing performance is correspondingly enhanced, effectively preventing medium leakage, which is particularly suitable for high-pressure environments.
Welded Butt-Weld Connection: The butt-weld end (BW) connection method enables the valve to closely integrate with the pipeline system, enhancing the integrity and tightness of the system. It also reduces the risk of leakage at the connection and improves the reliability of the system.
Carbon Steel WCB Material: The valve body is made of carbon steel WCB, which has good mechanical properties and corrosion resistance. It can maintain stable operation within a wide range of temperatures and pressures, with relatively low cost and high cost performance.
Flexible Wedge Structure: Equipped with a flexible wedge gate, it can automatically adjust the fit between the sealing surface and the valve seat, ensuring good sealing performance during valve opening and closing. At the same time, it reduces operating torque and extends the service life of the valve.
Non-Rising Stem: The non-rising stem design ensures that the stem does not rise during operation, saving space and facilitating installation and maintenance. It also avoids the risk of medium leakage caused by stem rising.
Multiple Operation Methods: It can be equipped with a manual gear operating mechanism, which is easy to operate. Suitable operation methods can be selected according to actual working conditions to meet the needs of different users.
Technical Parameters
Design Standard: API 600
Size: 1/2" ~ 48" (DN15~DN1200)
Pressure Class: 150LB~2500LB (PN20~PN420)
Valve Body Material: Carbon steel WCB
Bonnet Type: Pressure seal bonnet
Connection Method: Welded butt-weld end (BW)
Operation Method: Manual gear operation
Applicable Temperature Range: Generally -29℃ to +500℃, depending on the sealing material and working conditions
Applicable Media: Suitable for various media such as liquids, gases, and steam
Application Fields
This gate valve is suitable for high-pressure fluid transmission pipeline systems in industries such as petroleum, chemical engineering, natural gas, and electric power. It is especially applicable to occasions requiring high sealing performance and reliability, such as petroleum refining equipment, natural gas transmission pipelines, and chemical reaction systems. Its excellent performance and wide applicability make it an ideal choice in the field of industrial fluid control.
Quality and Testing
Manufacturing Quality: Strictly manufactured in accordance with API 600 and relevant international standards to ensure product quality and performance.
Testing Standards: Rigorous testing is conducted in accordance with API 598 standards, including shell strength testing and tightness testing, to ensure that each valve meets high-quality standards before leaving the factory.





