 |


| Quantity: | |
|---|---|
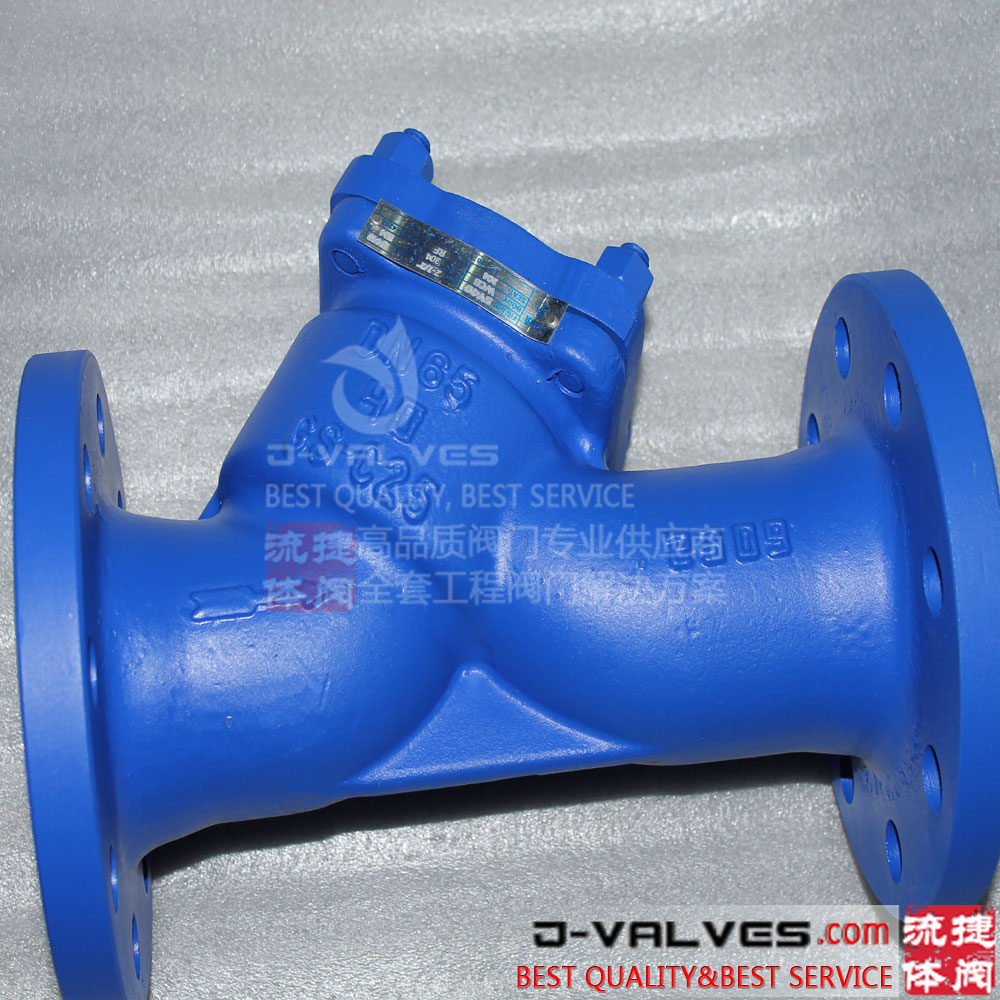
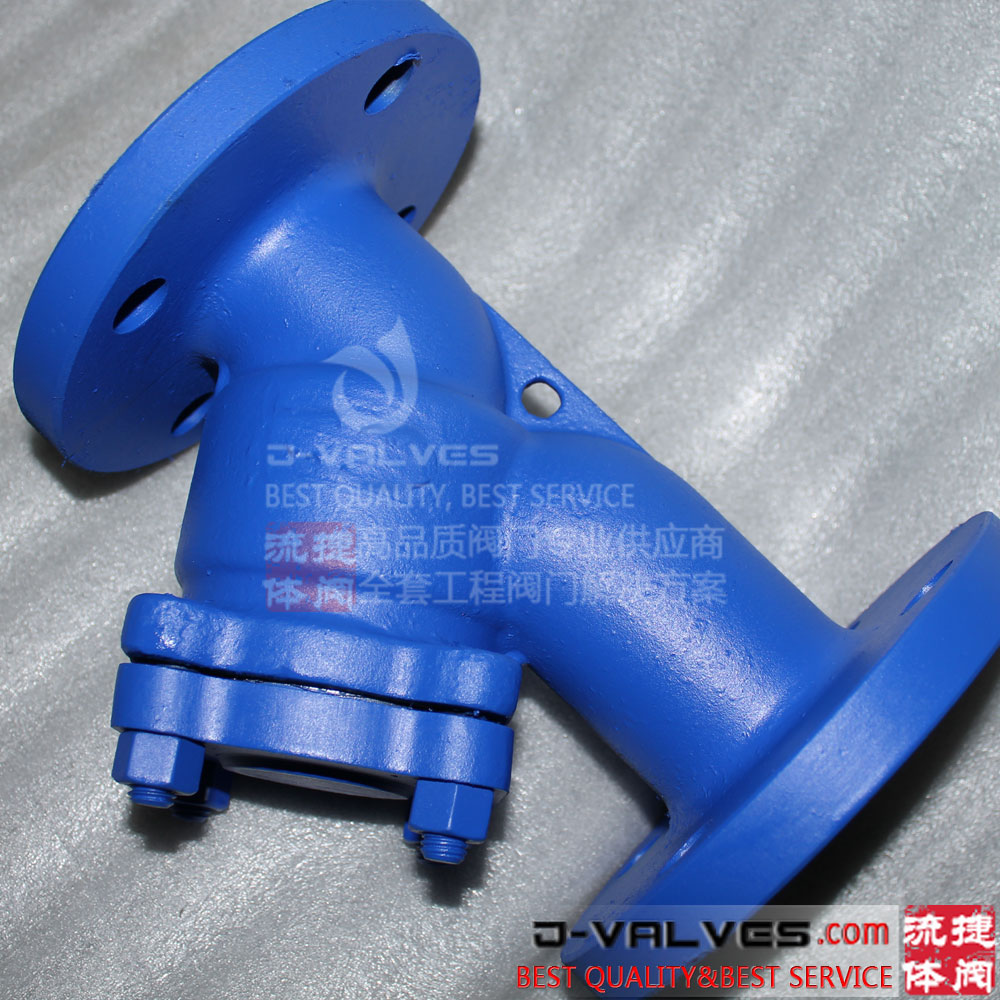
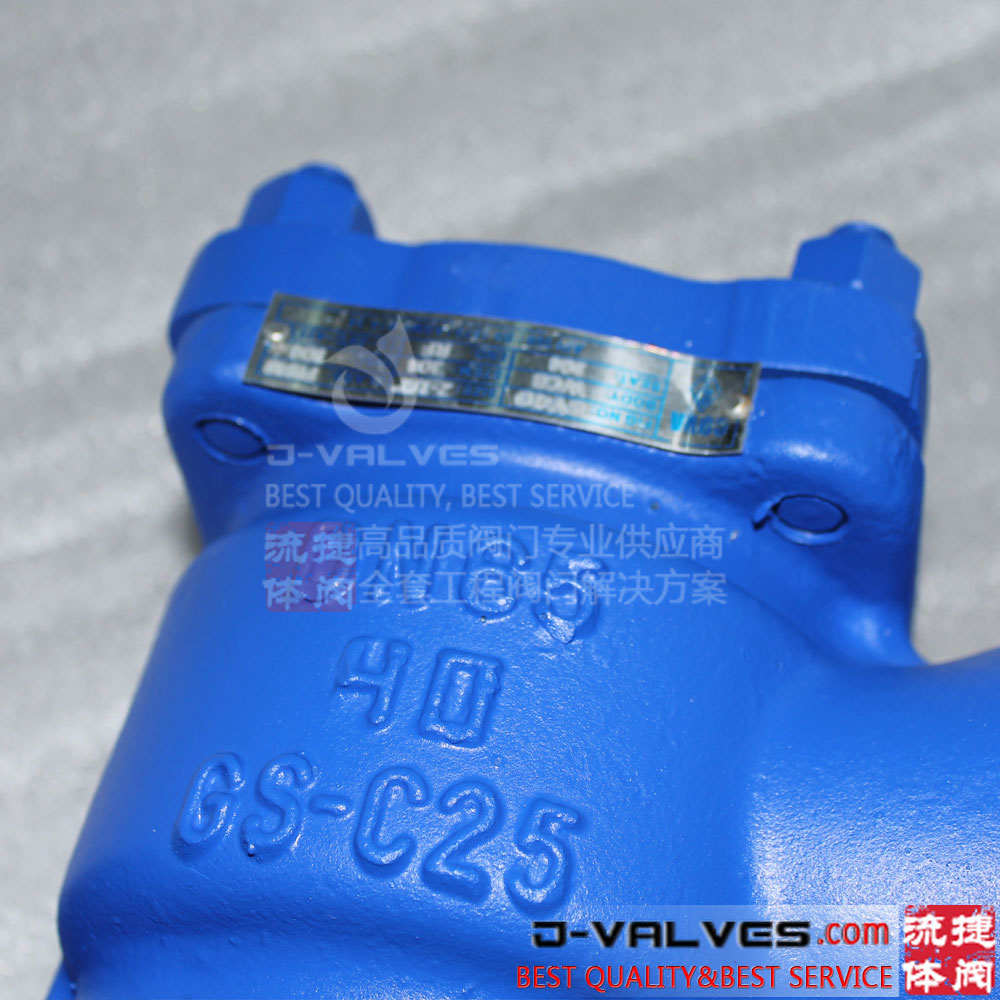
DIN Cast Steel Flanged Y Strainer
Main Features
Sturdy and Durable: Made of cast steel, it has high strength and good pressure resistance, can adapt to various complex working conditions and withstand relatively high working pressures.
High-efficiency Filtration: Equipped with a built-in stainless steel filter screen, it has high filtration precision and can effectively intercept impurity particles in the fluid to ensure the cleanliness of the fluid. The pore size of the filter screen can be selected according to different requirements to meet specific filtration needs.
Convenient Maintenance: The flange connection method facilitates installation and disassembly. Users can easily open the filter to clean or replace the filter screen without the need for complicated tools or equipment, which greatly reduces maintenance costs and time.
Strong Adaptability: It is suitable for a variety of media, such as water, oil, steam, gas, etc., and can be widely used in multiple industries such as chemical engineering, petroleum, pharmaceuticals, food processing, and energy.
Reliable Sealing: Equipped with high-quality seals to ensure no leakage under working pressure and guarantee the safe operation of the system.
Technical Parameters
Nominal Diameter: 1/2"~24" (DN15~DN600)
Working Pressure: 150LB~1500LB (PN20~PN260)
Working Temperature: -29℃~425℃
Filter Screen Material: Usually made of stainless steel materials such as SS304 and SS316, which have good corrosion resistance and filtration performance.
Connection Method: Flange connection, which complies with the DIN standard to ensure good connection and sealing with the pipeline system.
Application Scenarios
The DIN cast steel flanged Y-type filter is widely used in the following fields:
Chemical Industry: It is used to filter impurities in chemical raw materials, protect equipment such as reactors, pumps, and heat exchangers, and ensure the smooth progress of chemical production.
Petroleum Industry: In the processes of oil exploration, transportation and refining, it is used to remove solid particles in media such as crude oil and natural gas to prevent equipment blockages and damage.
Pharmaceutical Industry: It is used for fluid filtration in pharmaceutical production lines to ensure the purity and quality of drug production.
Food Processing Industry: It is used in production lines of beverages, beer, dairy products, etc., to filter impurities in fluids such as water and syrup, and ensure the safety and taste of food.
Energy Industry: In steam systems and hot water systems, it is used to filter impurities, protect equipment such as steam boilers and heat exchangers, and improve energy utilization efficiency.
Installation and Maintenance
Installation: During installation, it should be ensured that the flow direction of the filter is consistent with that of the fluid to avoid reverse installation. Meanwhile, check the sealing of the flange connections to ensure there is no leakage.
Maintenance: Regularly check the operating state of the filter. Depending on the cleanliness of the fluid and the frequency of use, regularly clean or replace the filter screen. When cleaning, appropriate cleaning agents should be used to avoid damaging the filter screen.
J-VALVES Note: All the data should be confirmed with the approved drawings of manufacturer.


Competitive Advantage:
On Samples Buyer bear the air fee, but this fee will be reduced from order directly
On After Sales Free replacement if there is any quality problem
On Delivery Never delay delivery time
On Materials Ensure material pure
Ensure material pure





