Views: 0 Author: J-VALVES Publish Time: 2026-11-04 Origin: Site


Every ball valve is a lever, a stem and a ball, and the interesting part is the two joints between them. A quarter turn applied at the handle becomes a torque in the stem, and the stem has to hand that torque to the ball through a shape: a pair of flats, a key in a keyway, a spline, a pin, a tongue in a slot. Each of those is a fit, and a fit is a place where motion can be lost or metal can be removed. Sizing the actuator is one question, and it has been covered elsewhere: how much torque the valve needs at breakaway, running and seating, and whether the actuator's output arrives intact at the top of the stem. This is the next question down the chain. When the torque does not arrive, which part gave way, what does the failure look like from the outside, and what can be seen before it breaks.
The small floating valve usually relies on a pair of flats machined on the stem end, either a single flat or two parallel ones, engaging a matching slot in the ball. It is cheap, it machines in one operation, and it is adequate for the torques involved at the small end of the size range, where the seat load rather than the stem decides the torque. Its weakness is wear: a flat loaded repeatedly in one direction rounds its corner, the slot opens up, and the play between them grows with every cycle.
The keyed joint uses a separate rectangular key seated half in the stem and half in the hub or the ball. It carries more torque than a flat of the same size, the key is cheap to replace, and it can be arranged so that the key is the part that fails. The splined joint spreads the same load over many teeth, which is why it appears on large trunnion mounted ball valves where the stem diameter is substantial and the torque is high; its cost is machining, and its failure mode is wear across every tooth rather than at one corner. A taper pin or a dowel is a positive lock that will not walk out, but it crosses the stem section and creates its own stress raiser, so it is usually a retention feature rather than the primary drive.
In a joint that has been thought through, the key is deliberately weaker than the stem. If the ball seizes, because of deposit, thermal growth or a seat that has been over-pressed, the key shears and the stem survives. That is a design intention, not a defect, and it is why a sheared key found during a strip-down is often good news: the cheapest part in the assembly did the job it was chosen for, and nothing expensive was twisted. The corollary is that the joint has to be built so the key can be replaced without scrapping the stem, and that the key has to be long enough to carry the load across its full length rather than on one end.
The opposite arrangement is the one that hurts. A key harder than the stem does not shear; it broaches its own keyway instead, cutting a wider, rougher slot as it rotates, and the stem is finished. A key that is too short engages only part of the keyway, so the same torque is carried on a fraction of the bearing area, and it fails under a load the design was supposed to handle. Neither fault appears on a drawing. Both appear when the valve is opened after a seizure.
The shear planes of a key are its two end faces, and the corner of the keyway is a stress concentration by geometry. If the key is a loose fit in the keyway, the load lands on a line rather than on a face, the corner of the key yields first, the key rocks slightly in its seat, and the next operation loads an already deformed part. The visible result is a handle that turns freely through part of its arc and then takes hold, and a valve that sometimes opens on the first attempt and sometimes needs a second. A shear that happens on a valve which was never loose is a different story: it points at a ball that stopped moving, and the seizure is the fault rather than the key.
A valve that is never cycled, or that sits in a line with vibration, still moves at the key. The amplitude is microscopic, the contact pressure is high, and the oxide film on the two steel faces keeps breaking and re-forming. The product is a fine red-brown powder that looks like rust and is not corrosion in the ordinary sense, and it is taken off both faces, so the fit opens up. Once the fit opens, every operation becomes an impact rather than a push, and impact loading accelerates the wear that caused it. Fretting is invisible from outside. Its early signatures are a small amount of lost motion plus dark or reddish debris in the grease at the stem, and it is the mechanism to suspect on a valve that has been in service for years without being operated.
On a trunnion valve the stem usually ends in a tongue that engages a slot in the ball, and the slot is commonly the softer of the two. Loaded always in the same direction, it wears into a ramp rather than a parallel slot. From that point the ball lags the stem: the stem rotates its full quarter turn, the ball rotates slightly less, and the difference is the amount by which the ball stops short of the seat. The valve still looks closed and the indicator still says closed. There is also an assembly version of this failure: if the tongue is longer than the slot is deep, the tongue bottoms out and holds the ball off the seat, which produces a leak that will be investigated as a seat problem for as long as nobody measures the slot. That misdiagnosis has a cost: replacing the seat restores nothing when the ball is stopping short of it, and the new seat is then blamed as well.
The stem is the one place on a ball valve where the pressure boundary and the atmosphere meet, and the keyway is a pocket just below the gland. Water that gets past the packing, or that condenses under a cold bonnet, collects there and stays. A carbon steel key in a stainless stem becomes the anode, the corrosion product has nowhere to go, and it packs the keyway until it jacks the key or seizes the stem. On insulated lines and on cold service the condensation is continuous rather than occasional, and the same pocket that holds water holds the debris from fretting, which keeps the moisture against the metal. This is the reason a stem assembly is worth inspecting at every strip-down even when the valve has given no trouble.
Every one of the mechanisms above ends in the same place, which is a few degrees of play between the stem and the ball. A few degrees sounds trivial and is not, because the whole travel is a quarter turn: a small angular loss is a real fraction of the stroke, and the last part of the stroke is the part that loads the seat. A manual operator feels it as a dead band before resistance. An actuated valve does not feel it at all. The limit switch is set on the stem, the position transmitter reads the stem, and the control room is told the valve is closed by the only part of the assembly that did reach the closed position.
What catches it is a measurement of the ball rather than the stem: a mark on the stem end and a matching mark on the ball or the body, checked against each other after a stroke; a seat leak test at the specified pressure; or the torque and current profile, where a ball that stops short shows as a seating torque that never arrives. The last of these is the practical one for a valve in service, and it is the same reading that a condition monitoring programme uses to separate a seat problem from a drive problem.
The table maps the chain from the handle to the ball. Read it from the top when a valve will not turn, and from the bottom when a valve turns but does not seal.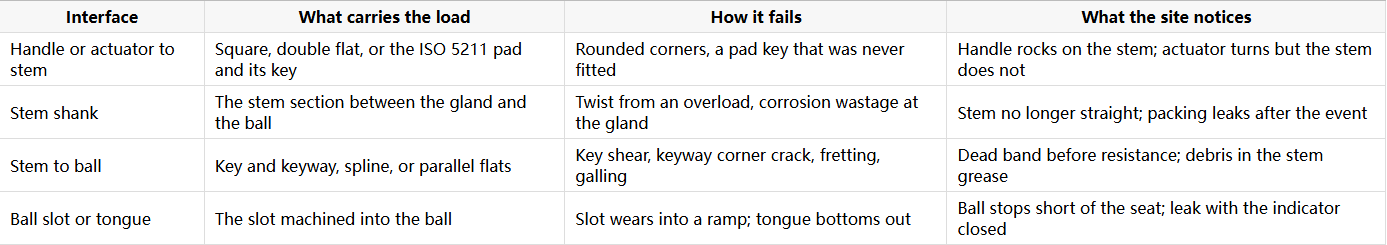
Four lines cover most of the risk, and none of them is a number to be guessed at the bench. State the drive arrangement by name, key and keyway or spline or flats, so that a substitute is a deviation rather than a surprise. State that the key is to be softer than the stem and retained against walking out, which fixes the fuse and stops the key from becoming a wedge. State the stem material with a certificate to EN 10204 3.1 and, where the service is sour, the NACE MR0175 requirement that goes with it, because a stem that fails a hardness rule fails it in the keyway first. State the mounting pad to ISO 5211 and require that it is concentric and square to the stem, since a pad that is off-centre loads the key in bending on every stroke.
Then require the functional check that the rest of this article is about: stroke the assembled valve and confirm that the ball reaches both positions, measured at the ball, not at the indicator. It takes a minute at the factory and it is the only test that catches a tongue that is too long, a key that is too short, or a slot that was machined in the wrong place. A valve that passes a shell test and a seat test can still fail this check, because both of those tests are done with the ball already in the closed position.
J-VALVES builds floating and trunnion ball valves from 1/2 to 56 inch (DN15 to DN1400), ASME Class 150 to 2500, with stem and ball materials certified to EN 10204 3.1, NACE MR0175 compliance where the service requires it, shell tests at 1.5 times and seat tests at 1.1 times rated pressure to API 598, and mounting pads machined to ISO 5211. Drive arrangements are agreed on the approval drawing before machining, which is the point at which a keyed joint can still be changed cheaply.
Is a sheared stem key a sign of a bad valve? Usually the opposite. In a joint designed with the key as the sacrificial element, a sheared key means the fuse worked and the stem, the ball and the seat were protected from an overload. What matters is why the ball seized, because that cause is still in the valve, and a replacement key fitted without finding it will shear again.
Why does my ball valve handle move a little before it grips? That dead band is lost motion somewhere between the handle and the ball. The usual causes are a worn key or keyway, a ball slot worn into a ramp, or a handle that never fitted its stem properly. It is worth measuring rather than accepting, because the same play that feels like a loose handle is the amount by which the ball stops short of the seat.
Should the stem key be harder than the stem? No. A key harder than the stem stops being a fuse and starts cutting its own keyway, which destroys the stem instead of a part that costs almost nothing. The intent is a key that shears before the stem yields, and that intent has to be written down, because two parts of similar hardness can fail either way depending on which one the fit loads first.
Can a worn key or keyway be repaired with the valve in line? Only on a design that allows the ball and stem to be reached without breaking the body joint, and even then the fit has to be re-machined rather than shimmed. On a welded body, or on a valve whose stem is inserted from inside, the repair is a workshop job. This is one of the reasons the body construction decision is taken during procurement rather than during maintenance.




